Why Typha attracts product interest
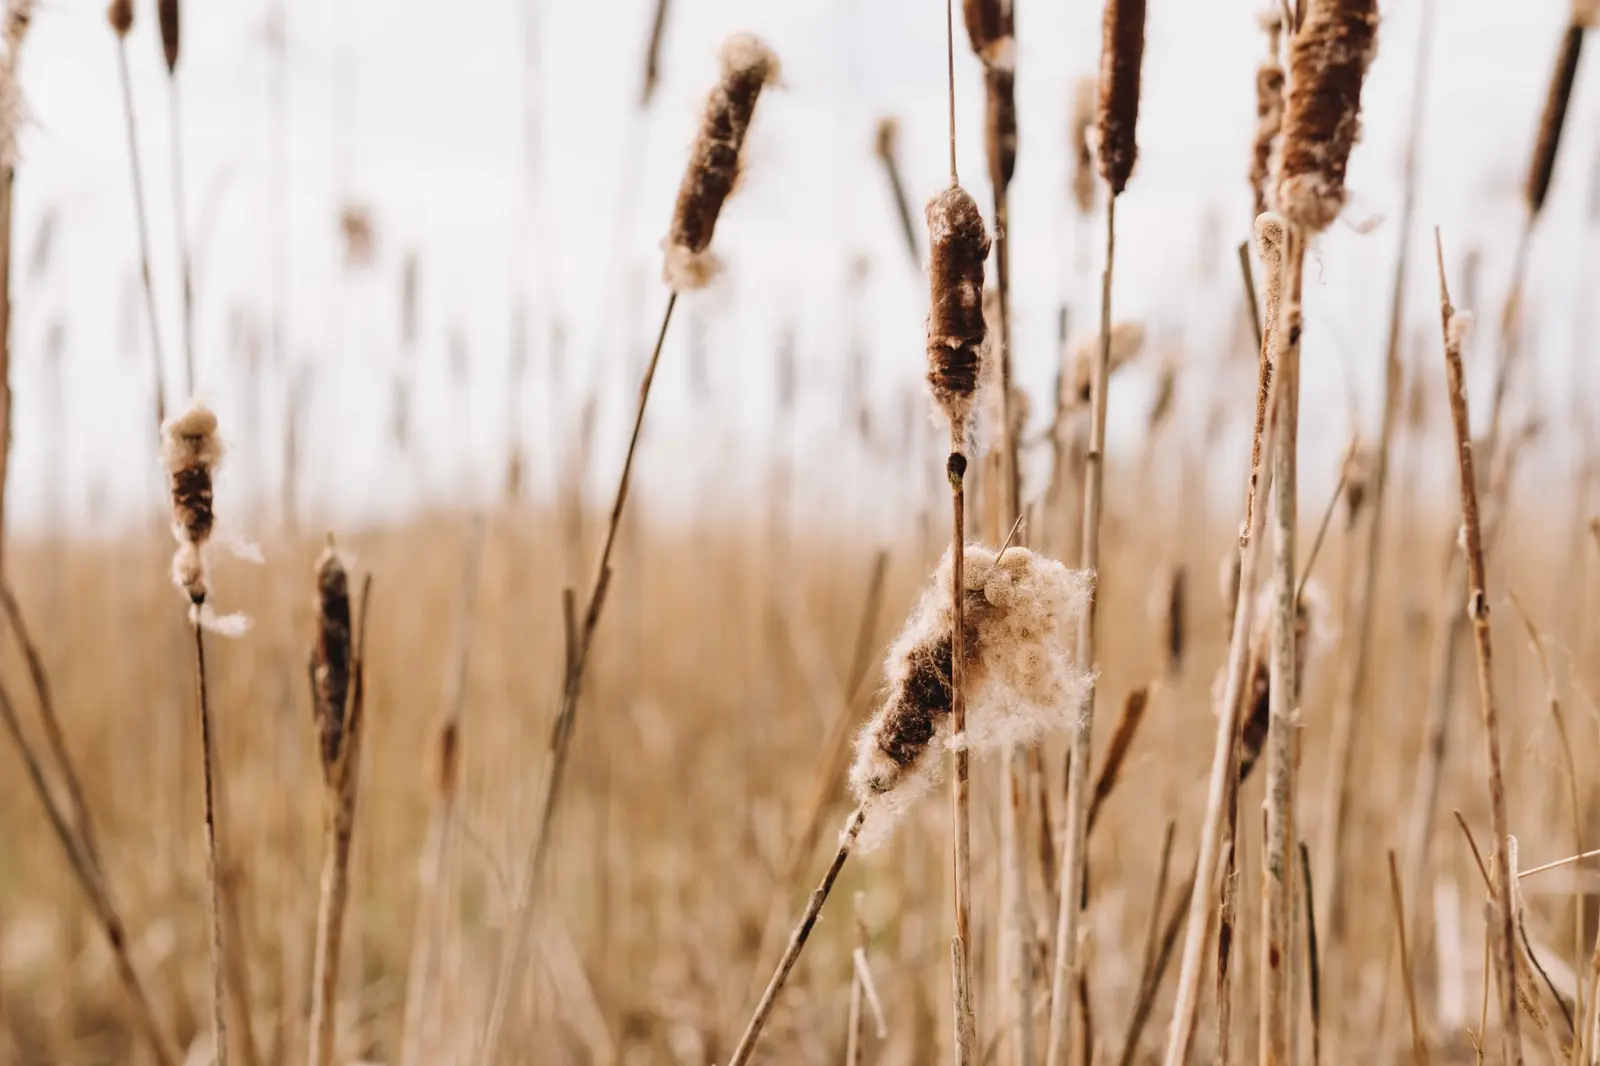
Typha—often called cattail, bulrush or reedmace—grows naturally in wet conditions. Its leaves combine reinforcing fibres with a lightweight, air-filled tissue. That structure helps explain why researchers have investigated the crop for insulation, boards and reinforcement rather than treating it only as fuel.
Fraunhofer Institute for Building Physics reported a magnesite-bound Typha panel with thermal conductivity of 0.052 W/mK, alongside sound, moisture and structural characteristics that justified further building trials. The same research also identified a central limitation: the panel had not moved into serial production.
A technically interesting crop becomes commercially useful only when a manufacturer can repeatedly turn it into a product that designers, contractors and regulators will accept.
Choose the product before optimising the crop
“Typha building material” is still too broad a proposition. A rigid internal panel, cavity insulation, door core, acoustic element and plaster reinforcement each require different fibre geometry, density, binder systems, moisture behaviour, fire performance and installation methods.
The first commercial decision is therefore not simply whether Typha can insulate. It is which product has a sufficiently valuable customer problem, a credible route to compliance and a manufacturing process that suits the crop.
The evidence a buyer will need
For a construction product, encouraging laboratory results are the start of qualification. The eventual evidence package may need to address thermal and acoustic performance, reaction to fire, moisture cycling, dimensional stability, biological durability, emissions, mechanical behaviour, installation and service life. The precise requirements depend on the proposed use and market.
Variability also matters. Water level, site conditions, harvest timing, plant maturity and storage could all affect the incoming material. A practical specification must translate that biological variability into acceptable ranges for the factory and the finished product.
What the commercial system has to connect
The business model must work across the entire chain: grower payment, water and land management, harvesting on wet ground, drying or conditioning, transport, particle preparation, binder addition, forming, quality control and sale. If one stage carries disproportionate cost or risk, good material properties will not rescue the proposition.
This is where Typha and miscanthus share common ground. Their physical structures differ, but both require a product-led development process. Each needs a defined application, controlled feedstock, economical conversion, appropriate testing and repeatable demand.
Our view
Typha deserves attention as more than “biomass from rewetted land”. The construction work already undertaken makes panels and insulation credible product directions. It does not yet make every Typha product commercially ready.
The next useful step is to select one product brief and work backwards from the buyer’s requirements. That creates a disciplined basis for material trials, manufacturing decisions, field cultivation and investment—and a much better chance that the crop reaches a real market.